
How orbital welding solution can be the right solution for you?
Orbital GTAW process can be applied to industries that require consistent and high quality weld joints with complete documentation of the welding process. It can be the right solution for pipelines where the weld job rotation is not possible or has very intricate pipeline design. The orbital weld head will be mounted close to such joints and the joints can be welded. Orbital GTAW process is also the solution for on-site welding applications where job rotation is not possible. As the documentation part is easily available from the power source, welding report analysis becomes an easy task.
Orbital GTAW process has a major advantage over manual GTAW. The advantage is repeatability of the process, data logging, flexibility of the designs that can accommodate any complex shaped pipelines, good control over weld parameters. The welding parameters are controlled through programming. The heat input is also controlled by using the pulsed orbital GTAW process. Sector-wise programming makes it easier to adjust the current or travel speed at6 O’clock position to mitigate the effect of gravity to attain a uniform penetration and weld bead. In order to increase production rates with consistent joint quality, orbital welding solution is the apt solution.
Orbital Welding solves a fundamental problem of lack of skilled welders. It overcomes the dependency on skilled workforce and shifts the focus on the larger production rates. The readily available documentation system and flexible weld head designing adds an edge to the technology.
Universal Orbital System has established itself as a leading orbital welding equipment manufacturers and known for the flexibility of designs, customized solutions catering to all industries. We are known for our research and development activities and our products are well designed to accommodate joints with higher complexity.
Orbital Welding: The building block of Data Centers
Orbital Welding advantages
Data centers are a necessity operating on industrial plants. The cooling systems and utility pipelines is an integral part of the data center industries. Data centers include CDUs (cooling distribution units), fire suppression, chillers, cooling towers. They are built using the SS pipelines that should be leak proof, higher strength joints, contamination free joints and manufactured with tight tolerances. In a surrounding where downtime can cause capital losses, joints need to be made with utmost precision; Orbital welding system becomes the most reliable solution.
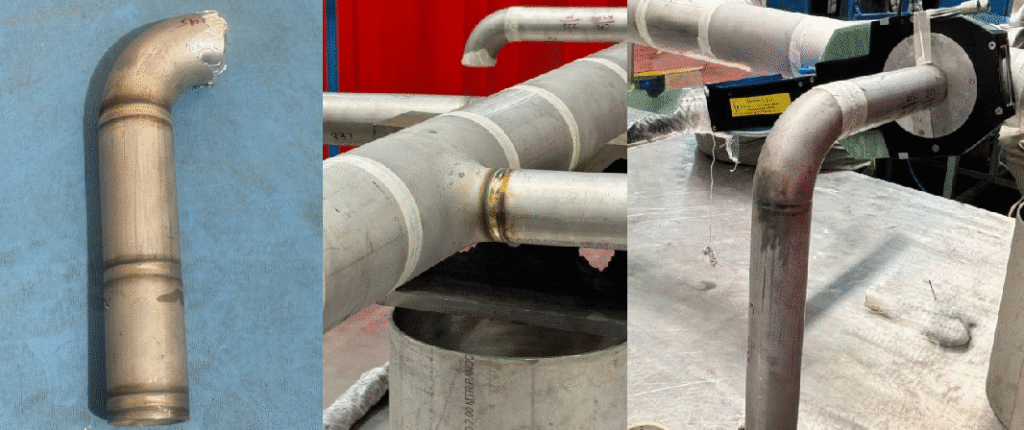
Orbital welding comes into picture where accurate welds, complex joint geometry, documentation and data acquisition requirements, repeatability, weld joints with 100% radiographic test results is a necessity. Orbital welding solution is applicable where the pipe rotation is not possible. Orbital welding solution can easily cover pipe to pipe, pipe to end fittings, pipe to short bend-long bend and pipe to tee.
Key features of Orbital welding useful for Data centers
- Consistent and repeatable weld joints
- Clean, contamination free weld joints internally and externally
- Compliance with weld joint specifica-tions can be met
- Weld joint traceability is possible
- Less chance of joint failures
Universal Orbital Systems solution for Data Centre pipelines:
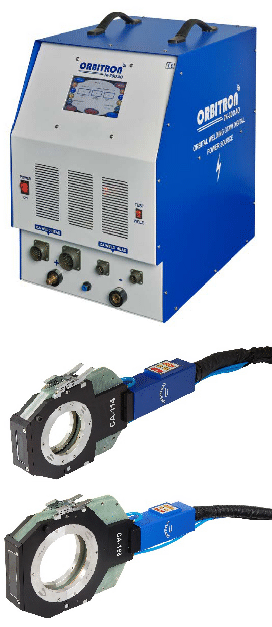
Universal Orbital systems have a solution suitable for Data center pipelines. We have closed arc weld heads CA-114 (range 1 inch NB to 4 inch NB) and CA-168 (range 2 inch NB to 6 inch NB) for NB pipes with thickness up to 3.5mm. The weld heads are specifically designed to accommodate the NB size pipes and end-fittings. The power source Orbitron 7K300 is provided with the weld heads. The programs are specifically designed and pre-set to accommodate NB sized pipelines. This product range is dedicated for NB based pipelines. The weld heads are compatible with step programming used to achieve 100% penetration with fusion orbital welding (single non-filler pass) for thickness from 3.00mm to 3.50mm. The addition of step programming facilitates the precise control of welding parameters and improves penetration for higher thickness tubes (in case of NB pipes). The pipes can also be welded using certain gas mixtures that can improve the weld bead geometry and aid to achieve uniform penetration with less heat input compared when used on 99.9995% Argon gas.
Along with orbital welding, edge preparation plays a crucial role in the success of an error free orbital weld joint. We have Orbital pipe cutting machine that can cut pipes/ tubes from 1 inch to 6 inch. The Orbital Pipe cutting machine ensures a 90-degree squared tube/pipe with no heat marks due to cutting and hence misalignment in the joint can be avoided. We also have tube facing machines to achieve the 90-degree squared tube/pipe and burr free edge.
Evolving Indian market for data centres
India’s rapid data centre growth, driven by cloud adoption, digital transfor-mation and government investment, is reshaping expectations for welding and fabrication. Projects are expected to have high skilled welding techniques with lowered downtime and repeatable joints. With a higher demand and continuous new development, automation in manufacturing is a necessity. The current Indian market is under a reform in manufacturing sector hence the standards are maintained at the utmost high level to ensure advanced technology develop-ment for data centre, global export of technology from India. Orbital welding is a promising solution for data centre industries which rely on consistency and clean internal-external surfaces.
Open Arc Weld Head Series
Open Arc orbital GTAW process refers to automatic pipe welding, where the pipe is stationary and the tungsten electrode orbits around the pipe. Here, the welding torch is visible and the weld head has a wire feeding system to weld from thickness above 3mm. The orbital weld head also has automatic oscillation system to mimic the welder’s weaving pattern. The weld head also has AVC (automatic voltage control) to control the gap of the torch and the pipe at all times during welding and cater to the ovality of the pipe.
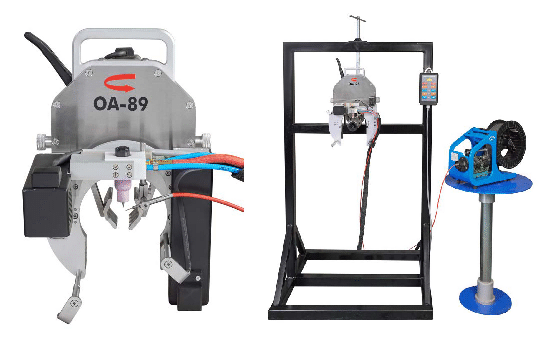
We have launched the open arc series in the month on January in the IMTEX Bangalore exhibition. Indigenously designed orbital weld head to cater the requirements of various industries. Currently, we are providing trials on our weld heads to various industries and ready for the market. We have worked on various pipe materials such as Carbon Steel, Mild Steel, SS and GI steel pipe. The pipe welding range is from 33mm to 89mm for OA-89 and 42mm to 125mm for OA-125. The trials were conducted on edge preparation as J-grove and V-grove.
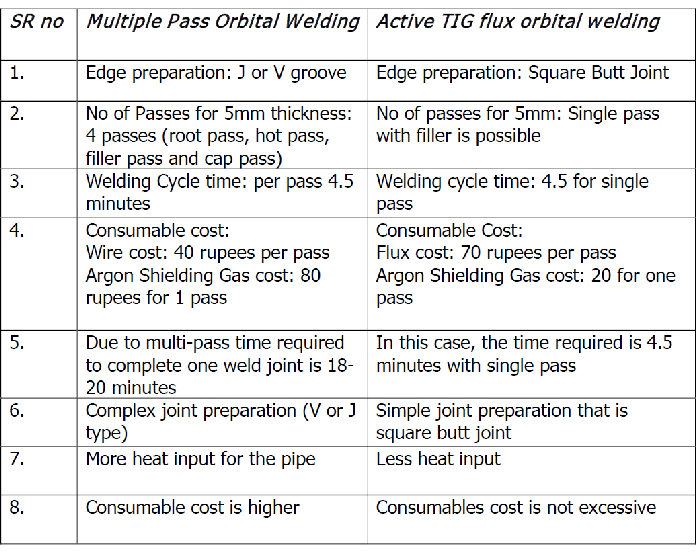
We have successfully completed trials of activated TIG flux on the open arc weld head series as well. In case of activated TIG flux, there is no requirement of complicated edge preparation such as V-grove (beveling). The edge prepara-tion required is square butt joint. The welding trials were successful and the joint was passed for Radiographic testing.
Experiments with Open arc orbital welding: Active TIG Flux orbital welding
Experimental details
MOC: SS-304
Diameter: 60.00mm
Thickness: 3.8mm and 5mm
Test carried out: Radiographic Test
Welding cycle time: 4.50 mins (pre flow- post flow)
Gas: Argon 99.995% pure
Weld Head: OA-125
Power Source: Orbitron 7K300
Edge preparation: Square Butt Joint
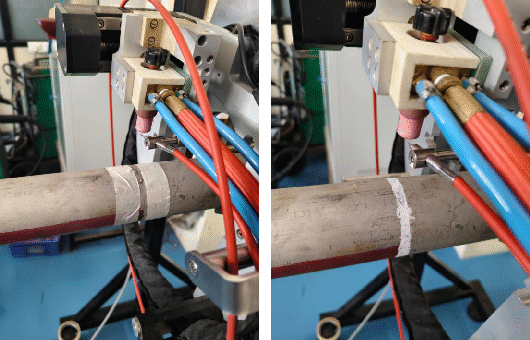
In the experiment, the active TIG flux was applied on the pipe that is to be welded. After application of the flux, open arc orbital welding was carried out on the pipe. The edge preparation was simple square butt joint. Full penetration was observed using the video boroscopy test. The type of welding was orbital active TIG flux with wire feeding
Observations and Results
Full penetration for 3.8mm and 5mm tube in fusion welding process
Constricted welding arc
Video boroscopy test passed
Uniform weld bead
Motivation behind developments in orbital welding
With the purpose of sharing and exchanging knowledge in the welding fraternity, the developments are planned and executed at Universal Orbital. Orbital Welding is a continuously evolving technology. We believe we can also contribute in the advancements of Orbital Welding. Universal Orbital is a research and execution oriented company that believes in simplifying the technology for practical usage and holistic knowledge approach.
Development of orbital welding equipment at Universal Orbital is fueled by the core purpose of welding automation of all kinds of designs of pipelines in various industries. The developments include WPS set-up for exotic materials like SS-310, Hastelloy, and Inconel etc. The development includes detailed study of welding parameters and achieving the required standard welding joint by mitigating material restrictions that causes welding defects. The development also includes designing various weld head, fixtures and collets to weld intricate pipelines while considering the production rates of the joints. The development extends to training that includes how to weld such joints with proper welding sequences.
Developing a welding solution which is collinear with the industrial advancements has always been the driving force at Universal Orbital Systems while considering a practical industrial approach. We are always open to conduct welding trials on complex pipelines and exotic materials to provide a practical, industrial solution.
Universal Orbital Systems Pvt. Ltd.
Web : www.orbitronsystems.com
